Top 10 Reflective Alu Foil Companies: Leading Manufacturers and Suppliers
2026-11-16
Most 'top supplier' lists for reflective aluminum foil are just paid advertisements in disguise, so it's hard to know which names actually hold up on a job site. Reflective foil has to balance high thermal performance with tear resistance, and a roll that fails early costs far more than its price tag. That's why we looked beyond the usual marketing claims and focused on companies with verifiable production capacity, consistent exports, and real-world performance feedback. From global manufacturers to agile niche suppliers, here are the top 10 reflective Alu foil companies worth shortlisting. One name that keeps appearing in recent sourcing discussions is Jinbo, especially for reflective insulation and house wrap foil. Read on for the full breakdown.
Where Reflectivity Begins in Modern Aluminum Foil Production
The first glint of reflectivity comes not from any coating, but from the final pass through the rolling mill. Aluminum foil is wound in a doubled sheet for the last gauge reduction. The outer faces pressing against the polished steel rolls pick up a near-mirror finish, while the inner faces, squeezed against each other, stay slightly dull. That contrast is set in seconds.
Roll surface finish, pressure, and lubricant film all decide how much light bounces back. A freshly ground roll leaves a different signature than one that has run for weeks. Mills adjust these variables depending on whether the foil is destined for heat shielding, packaging, or decorative use. Even tiny changes in reduction ratio shift the way the metal surface flows.
Alloy composition also matters before the foil ever reaches the mill. High-purity aluminum with low iron and silicon scatters less light at the surface, giving a cleaner reflection. Some producers add small amounts of elements to balance brightness against strength, accepting a slight drop in shine. The reflective character is therefore locked in upstream, not painted on later.
How Top Mills Keep Thickness Consistent Across Every Roll
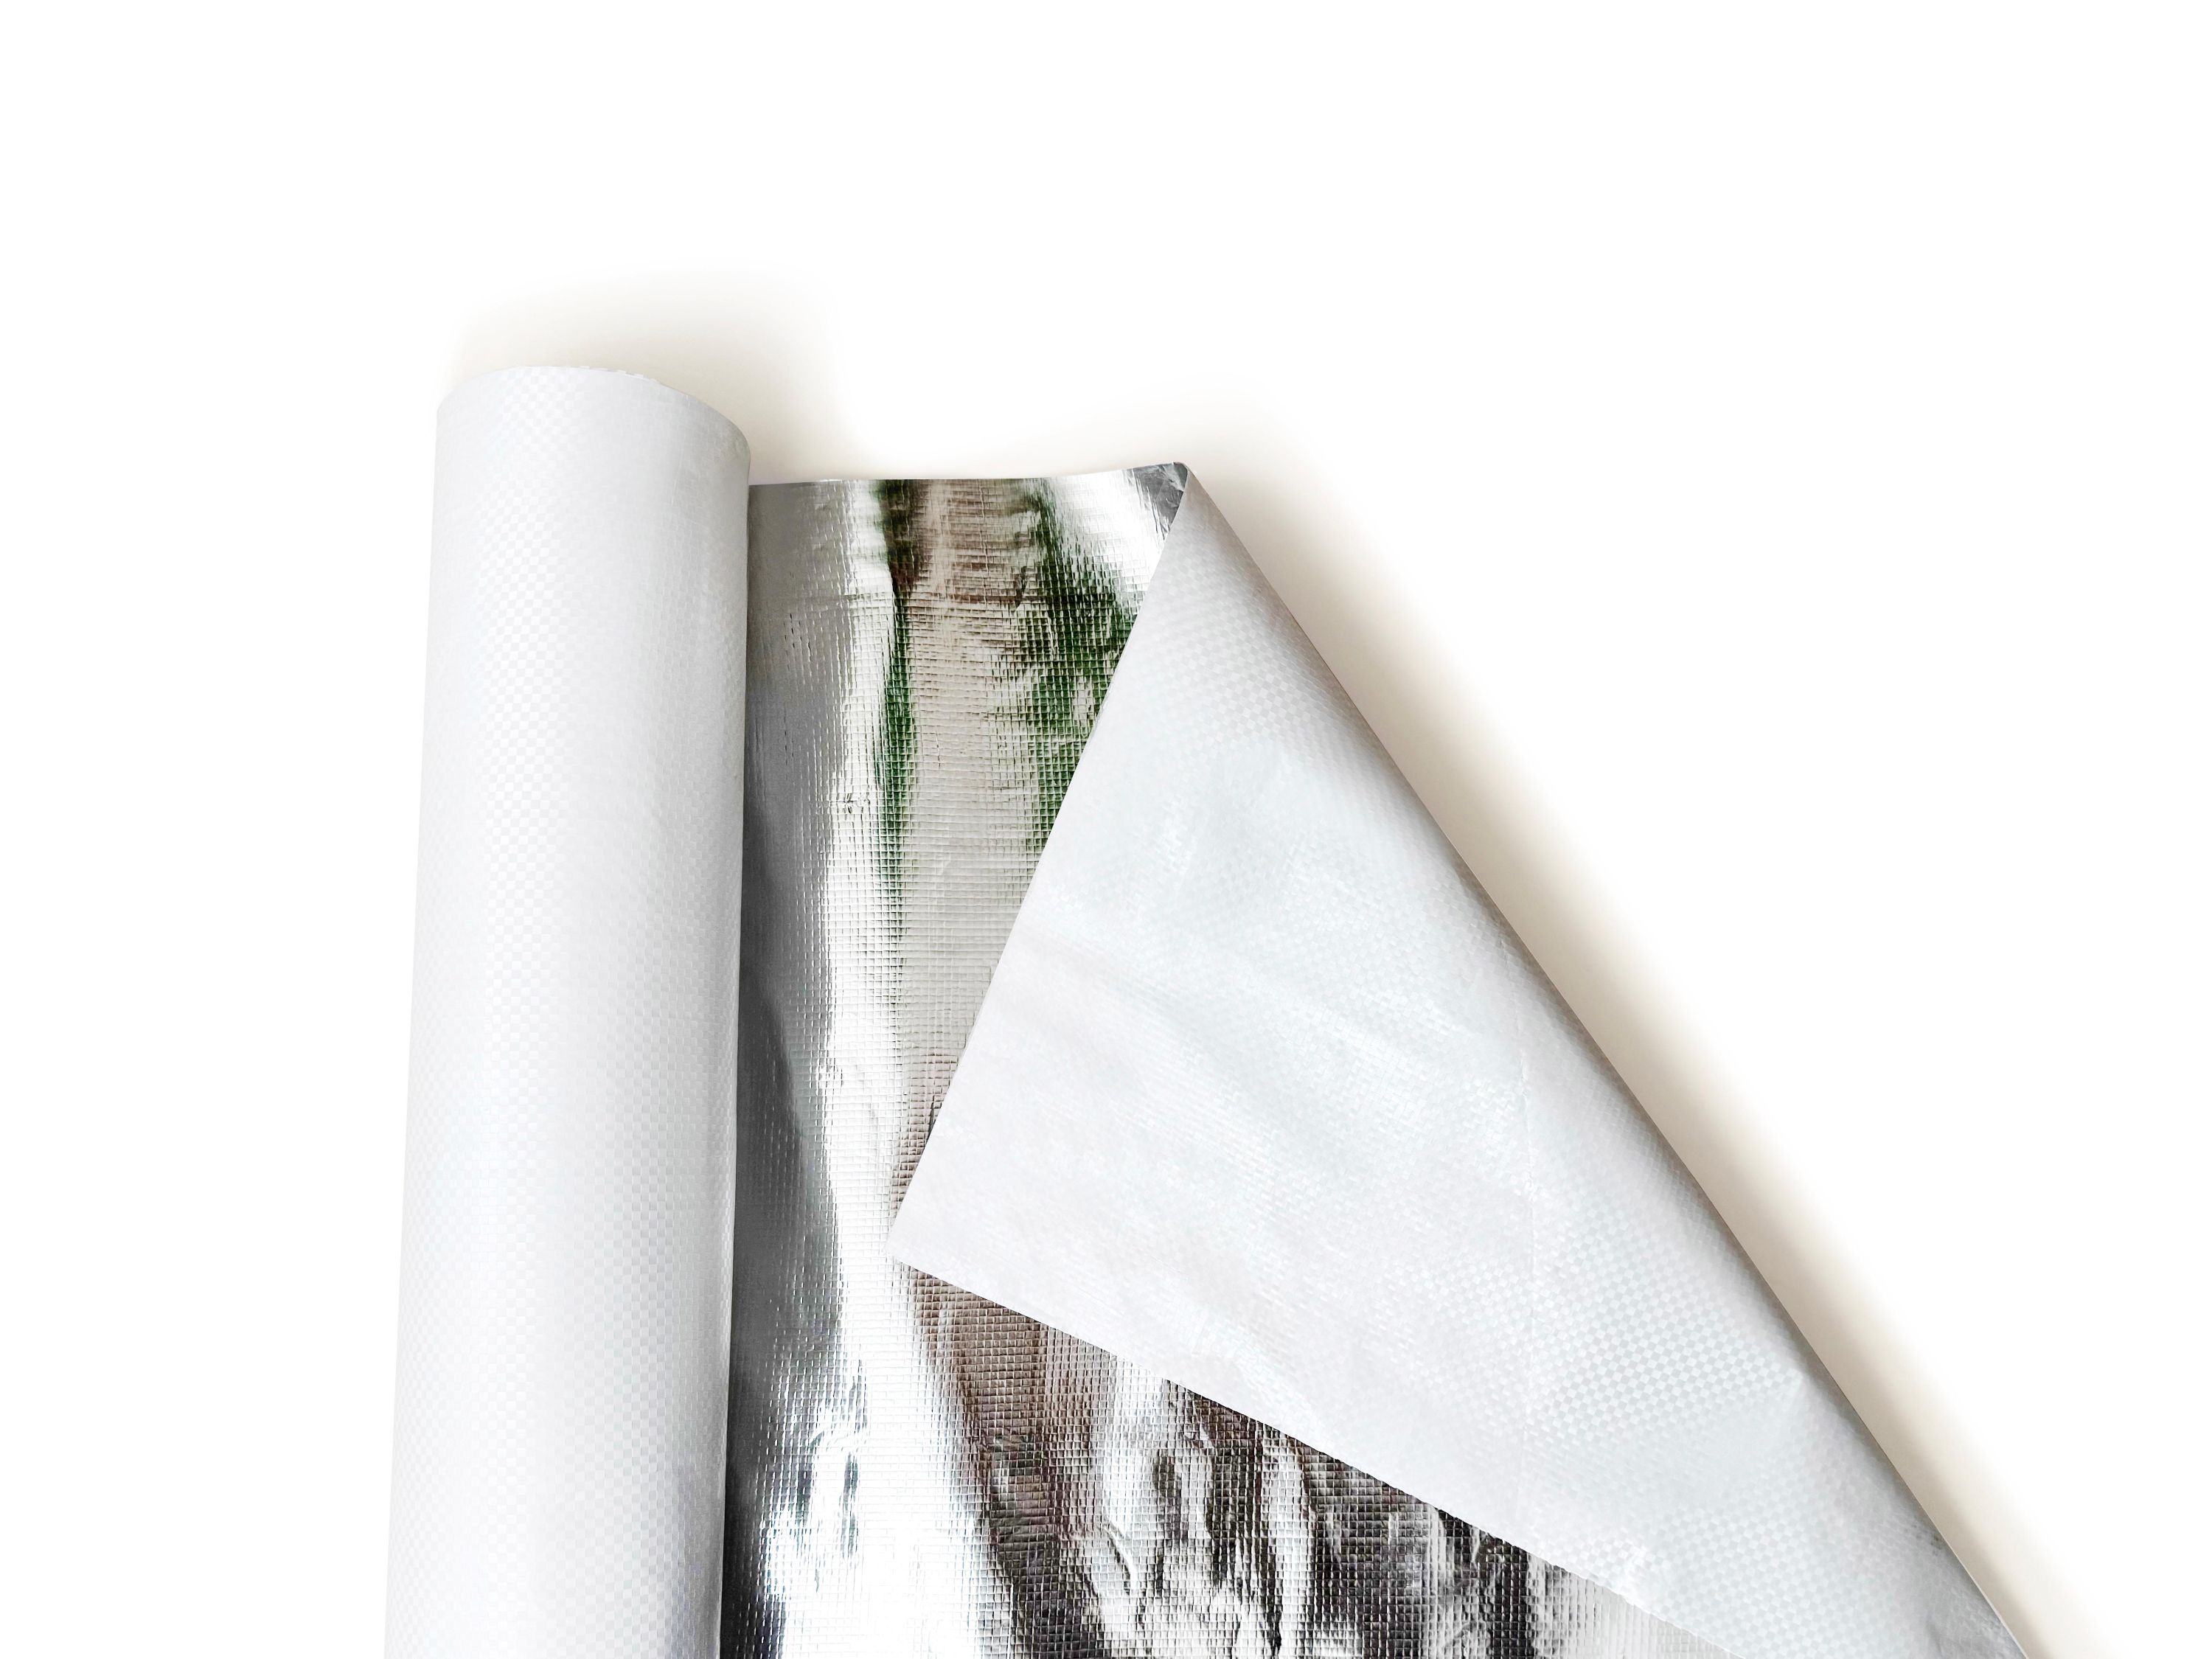
Modern rolling mills don't rely on a single measurement point or a generic feedback loop. Instead, they build a layered control strategy that starts with high-frequency laser or X-ray thickness gauges placed just after each roll stand. These sensors feed data into a dedicated automation system that compares actual thickness against the target profile up to a thousand times per second. The key difference at top-tier facilities is not just the speed of measurement, but how they use that data to predict deviation before it becomes visible in the strip. By combining real-time gauge readings with a physics-based model of roll force, elastic deformation, and thermal expansion, operators can adjust roll gap, tension, and rolling speed almost instantaneously.
Another hallmark of mills that achieve tight thickness tolerance is their approach to incoming material variation. Rather than assuming a perfectly uniform slab or coil, they map thickness and hardness across the entire incoming piece using automated inspection lines. This map is then fed forward into the mill's control system, so the roll gap changes preemptively as harder or thicker sections pass through. Combined with dynamic crown control and work roll bending, the mill can compensate for edge drop, center buckle, and local thickness spikes. Some advanced mills also employ model predictive control that runs multiple rolling scenarios in parallel, choosing the one that minimizes thickness error while respecting roll wear limits, lubrication constraints, and downstream coiling tension.
The final consistency layer comes from a tight integration between the mill's automation and its maintenance schedule. Rolls with even subtle surface defects can cause periodic thickness variation, so top mills track every roll's usage history, grinding pattern, and thermal profile. When a roll pair approaches its performance limit, the system automatically adjusts rolling speed or schedules a roll change before thickness drift occurs. Additionally, continuous statistical process control monitors thickness data across thousands of coils, flagging slow drifts in sensor calibration or hydraulic response that a single-coil snapshot would miss. This combination of predictive modeling, feedforward control, and long-horizon equipment monitoring is what separates mills that consistently hold thickness within a few microns from those that merely react to errors after they appear.
What Separates Reliable Suppliers in High Temperature Applications
Reliability in high-temperature supply chains doesn't come from a single certification or a polished catalog. It shows up in the details: how a supplier documents heat treatment of alloy batches, whether they test for creep resistance at the exact operating range you run, or if their technical team asks about your thermal cycling profile before quoting a part. Suppliers that hold up under these conditions tend to have deep metallurgical knowledge and a habit of pushing back when a material choice will shorten service life—even if that means losing a quick sale.
Another differentiator is transparency around sourcing and process control. A reliable partner can trace every cast, forging, or ceramic batch back to its original melt or powder lot, and they keep records that survive audits without scrambling. They also understand that high temperature isn't just about peak heat; it's about oxidation rates, dimensional stability after repeated exposure, and how joints behave when different coefficients of thermal expansion meet. The best suppliers will share test data on these factors instead of hiding behind generic spec sheets.
Finally, watch how a supplier handles failures or borderline results. Those who stand out treat a micro-crack found in a test coupon as a reason to recalibrate, not something to bury. They maintain accessible engineering support after the purchase, and their lead times account for re-validation when a heat or raw material changes. That combination of material honesty, record depth, and post-sale engagement is rare—but it's exactly what separates dependable high-temperature vendors from those who simply survive until the first thermal stress exposes them.
Regional Strengths That Shape the Global Foil Supply Chain
The global foil supply chain owes much of its resilience to the distinct manufacturing clusters scattered across a handful of regions. In East Asia, particularly China and Japan, the combination of low energy costs, continuous casting technology, and dense downstream packaging industries creates a volume-driven engine that can pivot quickly to shifting demand. This is not simply about cheap labor—it is about integrated production ecosystems where a new alloy recipe or thickness tolerance can travel from lab to rolling mill in days, not months.
Europe brings a different edge: precision and regulatory muscle. Germany, Italy, and France host converters that specialize in ultra-thin gauges for pharmaceutical blister packs and high-barrier food packaging. These players lean on recycled feedstock and stricter circular-economy mandates, which pushes foil producers toward closed-loop scrap systems and lower carbon footprints. The result is a premium supply tier where traceability and material purity outweigh raw output volume.
Meanwhile, the Middle East and India are rewriting the cost map. Access to subsidized energy, proximity to primary aluminum smelters, and aggressive export infrastructure allow these regions to undercut legacy producers on standard household foil and semi-rigid container formats. Their strength lies in scale of commodity conversion rather than niche engineering—but that scale is now large enough to set global benchmark prices and force legacy mills to rethink product mix.
Reading Between the Lines of a Supplier's Quality Claims
Suppliers often use phrases like "world-class quality" or "zero-defect rate" without explaining what those terms actually mean in their context. When you see such claims, dig into the supporting evidence: do they share real process capability data, or just a certificate from an audit that happened three years ago? A claim without a date, a standard number, or a measurable boundary is usually a marketing line wearing a lab coat.
Ask for the raw data behind the quality promises. Request a sample batch report that includes both the pass and fail rates across multiple production runs, not just the best one. If a supplier says they perform 100% inspection, ask whether that means every unit is functionally tested or just visually checked. The difference between those two interpretations can be the difference between a reliable partner and a costly rework cycle.
Pay attention to what the supplier doesn't say. A lack of mention about returned goods, customer complaints, or corrective action history often hints at selective transparency. Strong suppliers will voluntarily walk you through a past quality failure and what they changed as a result. That kind of candor is far more convincing than a polished slogan on a website.
The Quiet Shift Toward Closed Loop Recycling in Foil Manufacturing
For years, foil rolling plants treated their edge trims and off-spec coils as low-value scrap, shipped out or sold to secondary markets. That flow is quietly reversing. More manufacturers now run in-house remelt lines that feed clean scrap back into the same alloy stream, cutting both raw material purchases and external scrap logistics. The change doesn't show up in the final foil roll, but it reshapes the economics of every tonne produced.
The shift relies on better handling of thin-gauge scrap, which oxidizes quickly and picks up rolling oils. Instead of baling and hoping for a decent price, mills now use enclosed conveying, thermal de-coating, and induction furnaces tuned to preserve alloy composition. This lets them recycle foil waste that would previously have been downgraded into lower-value castings. Each tonne of internally recycled aluminium avoids the energy-intensive electrolysis step, so the savings are immediate and measurable.
Part of why this remains quiet is that closed loop recycling sits inside the plant, invisible to buyers and rarely mentioned in product sheets. It doesn't alter foil thickness, barrier performance, or appearance. For many producers, returning scrap to the melt is simply good operations, not a marketing story. Yet across the industry, these small internal loops are adding up, reducing primary metal demand and moving foil manufacturing closer to a genuine circular flow without any fanfare.
FAQ
Top companies usually run fully integrated operations from smelting to finishing, which gives them tighter control over grain structure and surface quality. They also maintain multiple rolling lines, so they can handle both trial runs and high-volume contracts without long lead times.
The field is fairly spread out. Germany, Italy, and France have a strong presence in high-end foil for technical applications. China and India dominate in volume and cost efficiency, while the United States and Brazil serve large domestic construction and packaging sectors.
Key specs include total reflectivity, alloy composition, thickness tolerance, tensile strength, and surface roughness. Buyers should also ask about emissivity values if the foil will be used in radiant barrier or thermal insulation systems.
They rely on in-line optical inspection systems, regular calibration of rolling equipment, and strict batch testing. Many also use statistical process control to catch drift early, so the last roll off the line reflects nearly as well as the first.
Absolutely. Many leading suppliers produce laminated structures that combine foil with kraft paper, polyester film, or bubble insulation. These composites improve tear resistance, moisture barrier properties, and ease of installation in building envelopes.
A common error is focusing only on foil thickness rather than actual reflectivity or emissivity. Some buyers also overlook surface oxidation during storage and shipping, which can degrade performance. Requesting sealed packaging and batch certificates can prevent these issues.
Energy codes are getting stricter, so more builders are using foil-faced insulation boards and radiant barriers. This shift favors manufacturers that can supply wide-format foil with consistent adhesion and low outgassing for enclosed wall assemblies.
Conclusion
The reflective performance of aluminum foil starts long before the final roll leaves the mill. Top manufacturers control alloy composition and rolling parameters to produce a surface smooth enough to bounce back over 85% of light, a figure that separates premium suppliers from commodity producers. Keeping gauge uniform across every meter is just as critical: advanced mills use laser-based thickness scanners and closed-loop hydraulic adjustments to hold tolerance within ±2%, preventing weak spots that compromise reflectivity or tear resistance. In high-temperature applications, such as automotive heat shields or industrial insulation, reliable suppliers distinguish themselves by providing foil that retains dimensional stability above 400°C without surface degradation. Buyers who dig into test data—not just marketing claims—quickly see which companies truly earn their place on a top ten list.
Regional capabilities also shape the global supply picture. Chinese and South Korean producers dominate volume with integrated smelting and rolling operations, while European mills lead in precision-coated foils for specialty lighting and aerospace uses. North American suppliers focus on fast-turnaround service and automotive-grade certifications. Beyond geography, the quiet shift toward closed-loop recycling is rewriting how leading companies source raw material: scrap from their own converting lines and customer returns is now re-melted and rolled back into foil, cutting primary aluminum demand by up to 30% in some plants. This circular approach not only lowers carbon footprint but also gives buyers a more stable cost structure. When evaluating the top ten reflective aluminum foil companies, the strongest contenders combine tight process control, honest quality documentation, regional logistics advantages, and a genuine commitment to material recovery.
Contact Us
Contact Person: Miranda
Email: [email protected]
Tel/WhatsApp: +8615231299719
Website: https://www.ihousewrap.com/